Prime or Standby: Choosing a Duty Rating for 24/7 Power
The same engine can be sold at three different ratings. Picking the wrong one either wastes capital or shortens engine life — and the difference is measured in hours per year.
Starting a set and watching the voltage settle proves almost nothing. Here is what a 25 / 50 / 75 / 100 % load test actually measures, and which faults only appear under load.
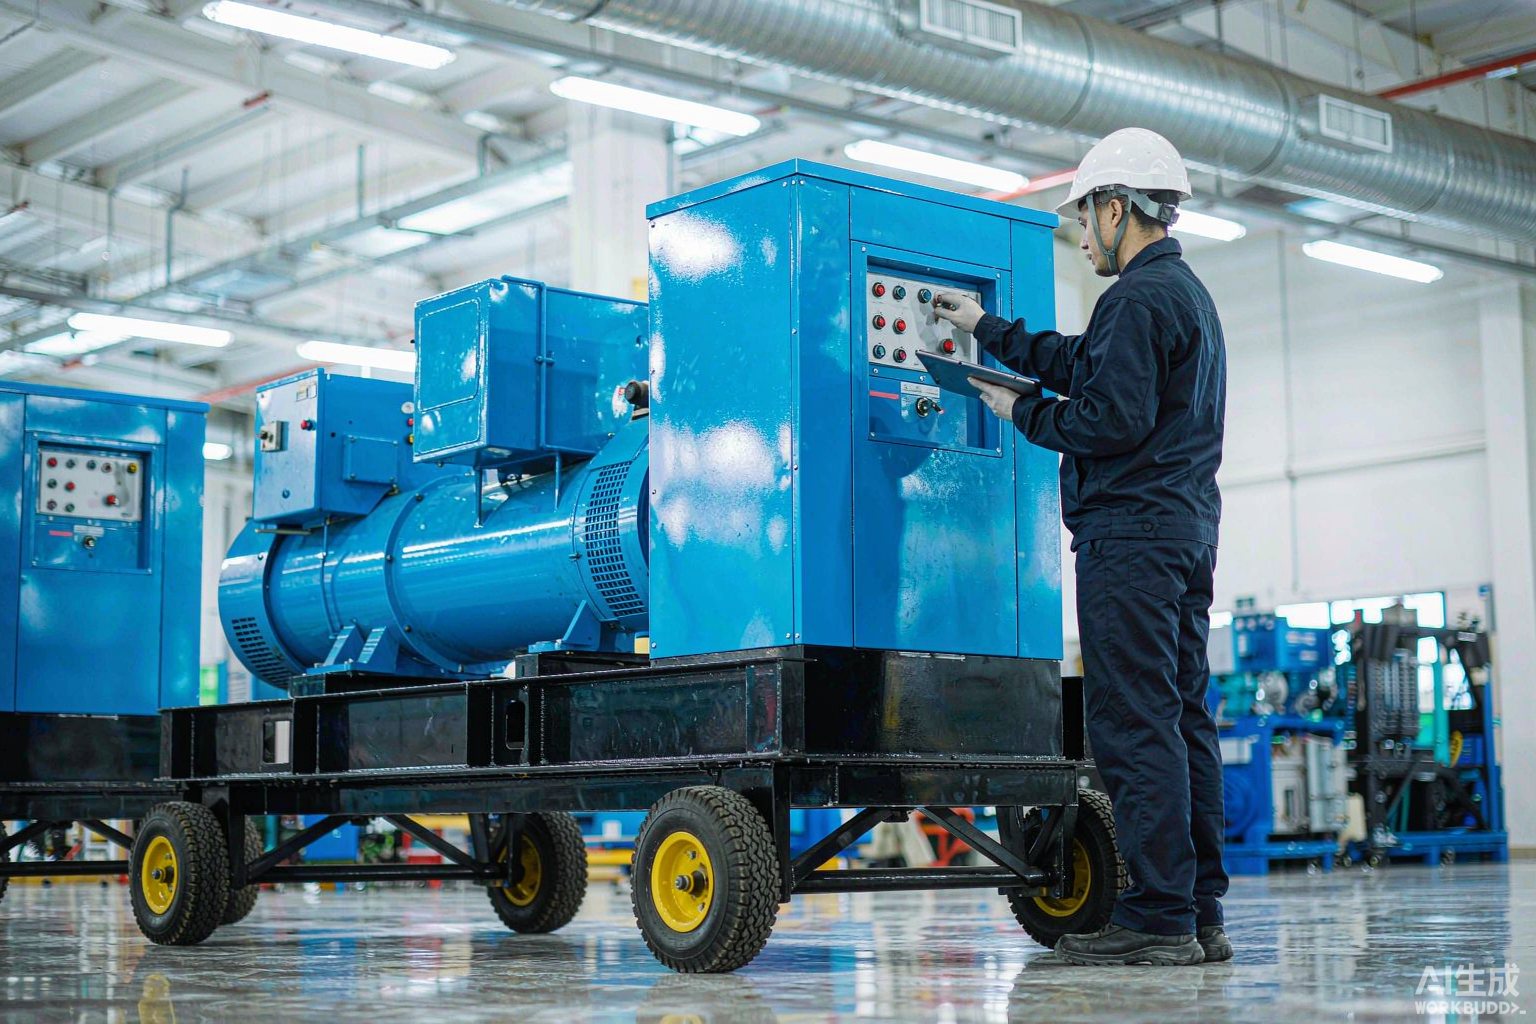
A generator that starts, idles and holds 400 V on a meter has passed the easiest test in the book. The failures that cost money on site — a governor that cannot accept a step load, a radiator that was sized for a cooler day, a breaker set below the alternator rating — stay hidden until the set is carrying a real building.
At no load, the engine is doing very little work. Fuel delivery is at its minimum, the turbo is barely spinning, coolant flow is at its lowest, and the alternator is producing only excitation current. Almost every component that fails in service is comfortably inside its limits in this state. Running a set unloaded for ten minutes tells you the wiring is correct. It does not tell you the machine will hold a hospital at 02:00.
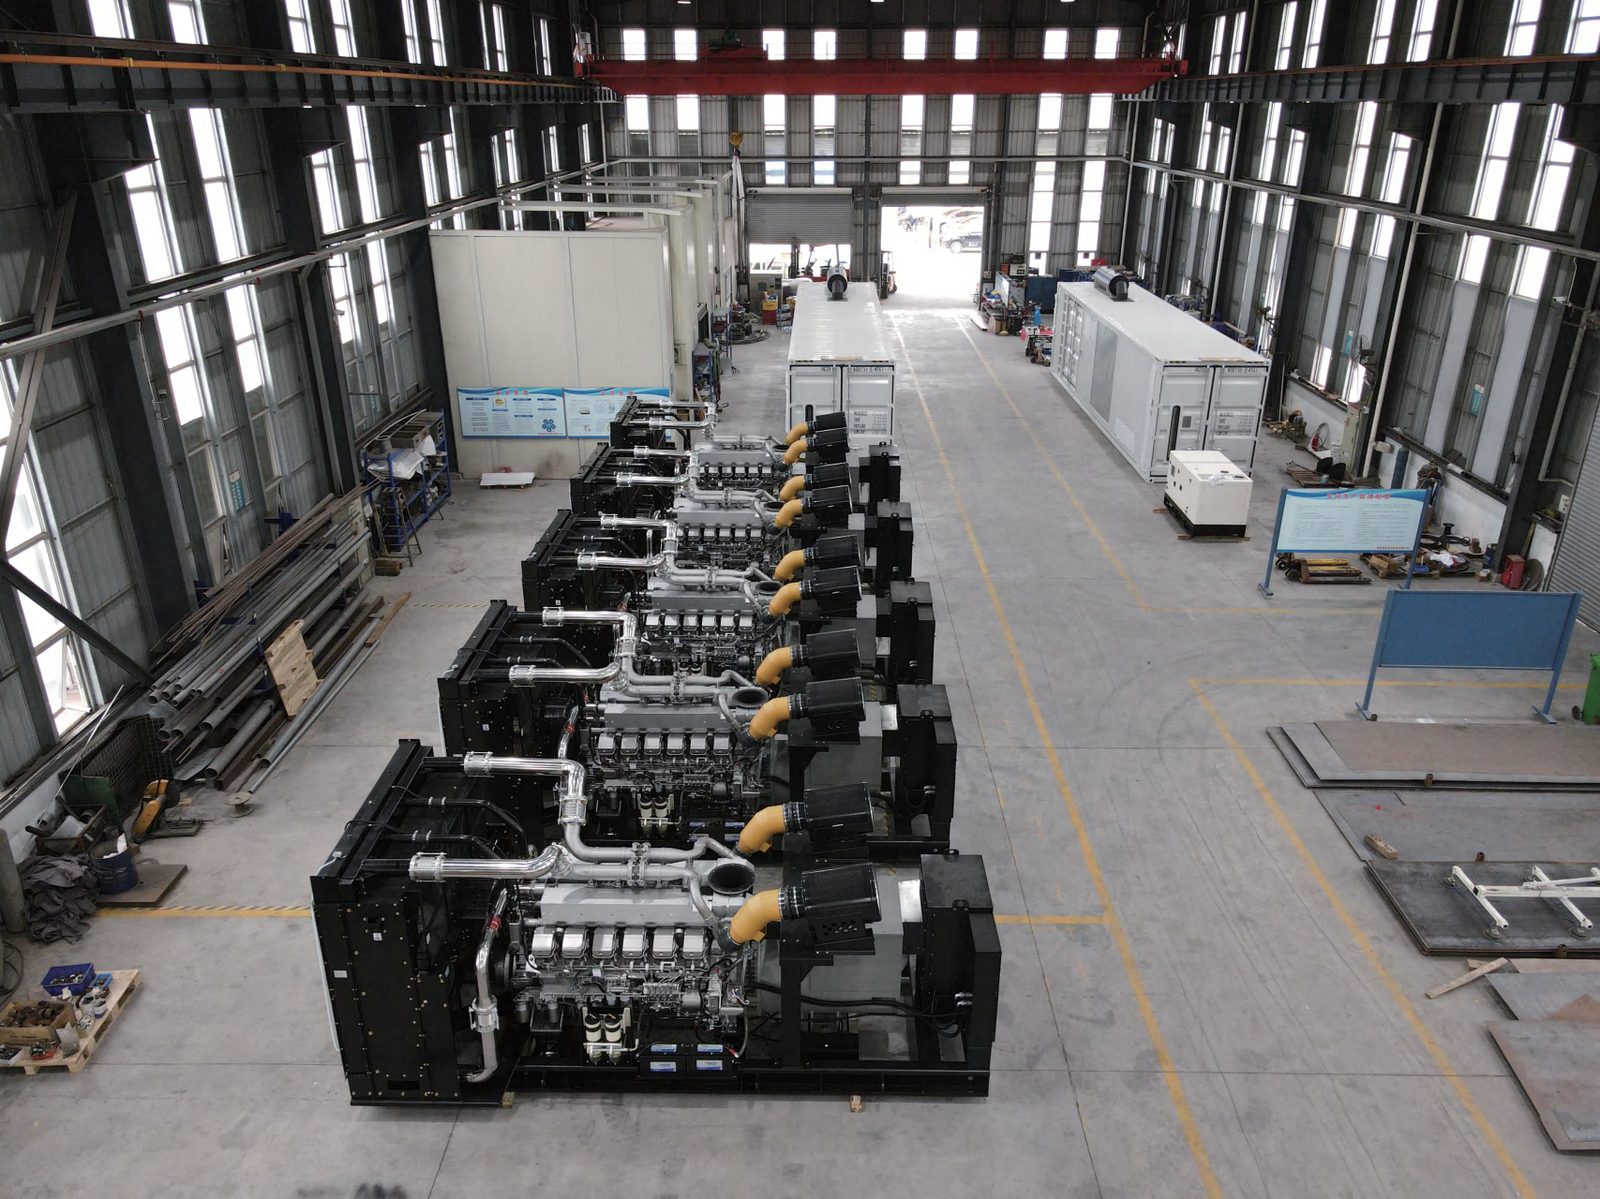
Cunmi runs every set through four resistive load steps before it is packed. Each step is chosen because it exposes a different class of fault.
| Load step | What it is really checking | Typical fault it exposes |
|---|---|---|
| 25 % | Light-load stability, fuel/air ratio at low delivery, exhaust temperature spread | Hunting, uneven cylinder contribution, injector imbalance |
| 50 % | Transition through the turbo's inefficient band, cooling under part load | Boost leaks, thermostat opening late, fan drive slip |
| 75 % | Thermal margin, oil pressure at working temperature, alternator winding rise | Undersized radiator, blocked charge-air cooler, low oil pressure when hot |
| 100 % | Rated output, governor droop, breaker and protection settings, fuel consumption | Droop outside ISO 8528 G2/G3, protection tripping below rating, fuel starvation |
Twenty minutes at each step is enough for temperatures and pressures to stabilise. A set that only sees a two-minute bump at full load never reaches thermal equilibrium, so the most expensive faults — the ones that appear after forty minutes of running — are never triggered.
Prime-rated sets are expected to carry a 10 % overload for one hour in twelve. We verify that capability rather than assume it: a short block at 110 % confirms the engine has fuel headroom and that the protection curve does not trip inside the permitted window. A set that trips at 105 % will fail the first time a chiller bank restarts.
A load test is only useful if it produces a record. For every Cunmi set we issue a test sheet carrying the serial numbers of engine and alternator, the four load steps with voltage, frequency, current and power factor at each, coolant and oil temperature at stabilisation, fuel consumption at 100 %, protection settings as left, and the signature of the technician who ran it. That sheet is what an installer needs when the commissioning engineer asks whether the machine has been proven.
No. A factory acceptance test is a broader document that can include dimensional checks, wiring inspection, protection calibration and witness testing by the client. The load test is one chapter of it. For export orders we can arrange witnessed testing with remote video if the buyer cannot travel.
Yes, with a rental load bank, and it is worth doing at commissioning on critical installations. The difference is timing: a fault found in our bay is a scheduling problem; the same fault found on site is a delay, a crane, and a conversation with the client.
Every configuration is tested in its final enclosure, because the enclosure is part of the thermal and acoustic system. Testing an open set and then fitting a canopy proves nothing about the package the customer receives.
The same engine can be sold at three different ratings. Picking the wrong one either wastes capital or shortens engine life — and the difference is measured in hours per year.
Buying the next size up feels safe. In practice it moves cost from the capital budget into fuel, maintenance and premature engine wear — and it rarely improves reliability.
Low-load running looks gentle on the machine. In reality it is one of the fastest ways to glaze bores, load a DPF with soot and double your maintenance bill.
Send the load schedule, site conditions and destination port. We answer technical questions directly, usually within one business day.